


Grinding and polishing is a common hardware processing technology. Most of the hardware parts need to be used. However, many people do not know which steps to polish. What is the specific process? Today, the technology of smiling and technology will give you a hand-on-plate model polishing process.
Rough polishing: you can choose to polish with a polishing machine. The common methods include removing burr on prototype model by grinding wheel, small sand hole and small scratch mark. There are two kinds of specifications of grinding wheel: φ 400mm wheel is better used in rotating body, φ 300mm wheel is used in prototype parts. After coarse throw, use oil stone grinding, with strip oil stone plus lubricant or coolant.
Semi-fine throw: mainly use sandpaper and lubricant. Grinding wheel is used and sand paper is used to remove the omissions of grinding wheel so that the wear marks on the surface of the whole parabolic body are finer and smaller, and the grinding marks are balanced and consistent. When polishing, the rotating body should be in accordance with the direction of whipping, and the polishing direction of the prototype should be crossed with the tapping direction of the grinding wheel.
Fine polishing: the diamond grinding paste is mainly used. The diamond grinding powder or the grinding paste is ground with a polishing cloth wheel, typically in the order of a small to a large number, a diamond grinding paste and a polishing cloth wheel can be used to remove the hair-like wear marks left by the sandpaper, and then the polishing is carried out with the adhesive felt and the diamond grinding paste in order of from large to small. The precision is required to be carried out in a clean polishing chamber in a processing plant at a polishing process of 1. m u.m or more, and an absolute clean space is necessary for more precise polishing, since dust, smoke, dandruff and water foam are likely to be discarded after high-precision polishing.
Refinement: 1. Sand paper is used to remove the omissions of grinding wheel, so that the grinding marks on the surface of the whole parabolic body are finer and smaller, and the grinding marks are balanced and consistent. The direction of beating should be the same as that of grinding wheel, and the direction of beating of prototype should be crossed with the direction of beating of # grinding wheel. 2. With grinding wheel and a small amount of green ointment, remove the scratches after grinding wheel processing, so that the body to the naked eye does not appear to have obvious scratches, the surface is balanced and consistent, touch with the hand has a soft feeling. Apply a small amount of green ointment evenly on the grinding wheel to further eliminate the small marks left by the wheel so that no scratches can be seen on the body of the wheel.
Mirror treatment: a pre-treatment with a linen wheel with white oil paste to make the surface of the parabolic body have a sense of dark light. Finally, a cloth wheel is used for pumping to achieve the mirror effect. The pulley should be full of ointment when beating, so that the wheel has a sense of softness, the strength must not be too large when beating, so as not to cause the discoloration of the body, at the same time, it is necessary to check the wheel slices regularly in the process of beating, properly arrange the long cloth hair, and make the cloth wheel smooth.
Sub-light treatment: the first four-step treatment is the same as the mirror light treatment, that is, after adding fine Ⅲ treatment, the sub-light wheel can be processed.
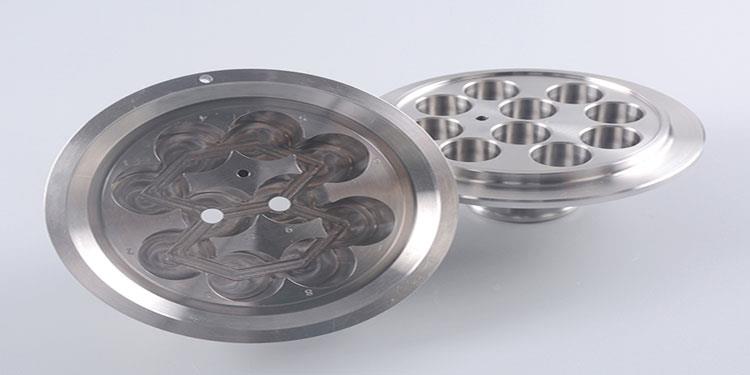
If you want to know more about cnc lathe aluminum prototype service and aluminum auto wheels 5 axis cnc mill . please email below.
steven@smilecnc-china.com (our sales manager)


